Comprehensive audit and refurbishment of a reverse osmosis membrane system relocated from Sydney to Melbourne. APP restored performance by optimising recovery, modifying CIP regimes, and fine-tuning controls. Client now benefits from maximum salt rejection and reduced operational costs.
- Home
- APP Blog
- Case Studies
- A SUCCESSFUL AUDIT OF INDUSTRIAL REVERSE OSMOSIS PLANT
A SUCCESSFUL AUDIT OF INDUSTRIAL REVERSE OSMOSIS PLANT
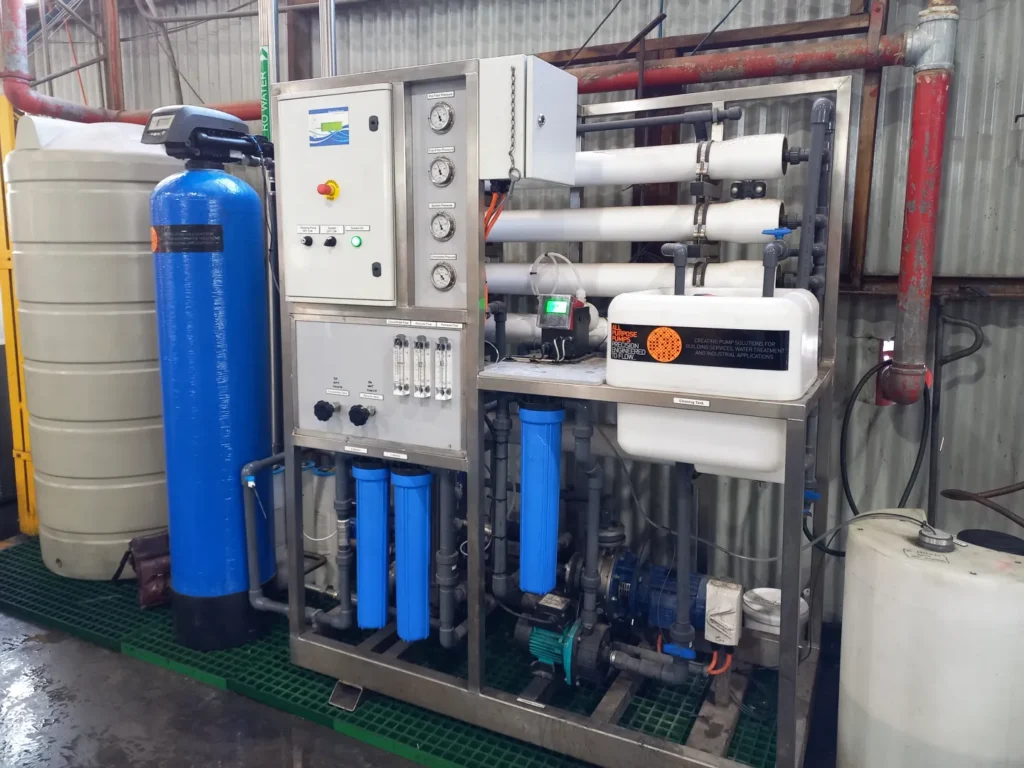
Comprehensive audit and refurbishment of reverse osmosis membrane system for industrial application in Melbourne’s western suburbs.
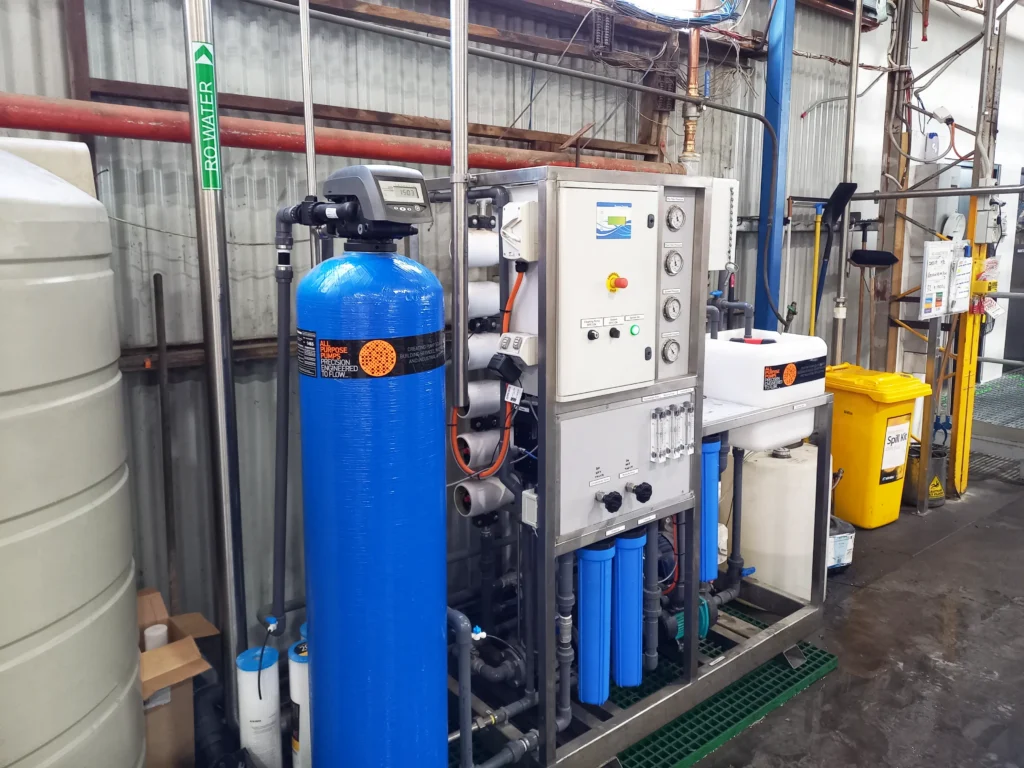
All Purpose Pumps was recently approached to audit and consider the requirements of refurbishing a reverse osmosis membrane application to be utilised in an industrial application in the western suburbs of Melbourne.
APP visited the site and learnt that the plant had been purchased from a site in Sydney designed for Sydney mains and was later relocated to Melbourne. Since water mains in Sydney are different to Melbourne water mains, this plant was not suitable and as a result, it didn’t perform correctly. The plant had a poor history of failing to meet the site requirements as permeate flow was inconsistent, membrane performance was poor, overall process balancing was not efficient, membrane cleaning was non-existent which had left the customer on the verge of scrapping the plant altogether.
All aspects were audited by APP:
- Feed water systems
- Pre-treatment
- Antiscalant
- Control system and PLC
- Instrumentation
- Hydraulic balancing and performance optimisation
- Clean in Place (CIP)
- Operations and Maintenance
After generating a plan and proposal to suit the application and the customer’s production schedule, APP began works on site. The works carried out restored performance in maximising recovery and rejection whilst maintaining consistent operational performance. The CIP regime was modified to obtain maximum possible membrane recovery post cleaning and the control system was interrogated and adjusted with careful attention to fine tuning. The antiscalant system was modified and fine tuned to suit Melbourne Mains.
There are still some further works to be undertaken on the pre-treatment.
CLIENT BENEFITS
The Client now receives the benefits of:
Maximum long-term sustainable salt rejection and recovery
Lower operational costs
Less downtime
Consistent, trouble-free operation
Permeate production to meet the site needs
The advantages of APP’s more than three decades of experience with industrial applications for membrane separation processes across all industries and applications.
get in touch
thanks for your submission!
We’ve received your enquiry and a member of our team will be in touch shortly. Whether you need product advice, technical support, servicing or a project quotation, we’re here to help and look forward to assisting you.